Series 16i / 18i Additional Manual Page 4
Additional Manual
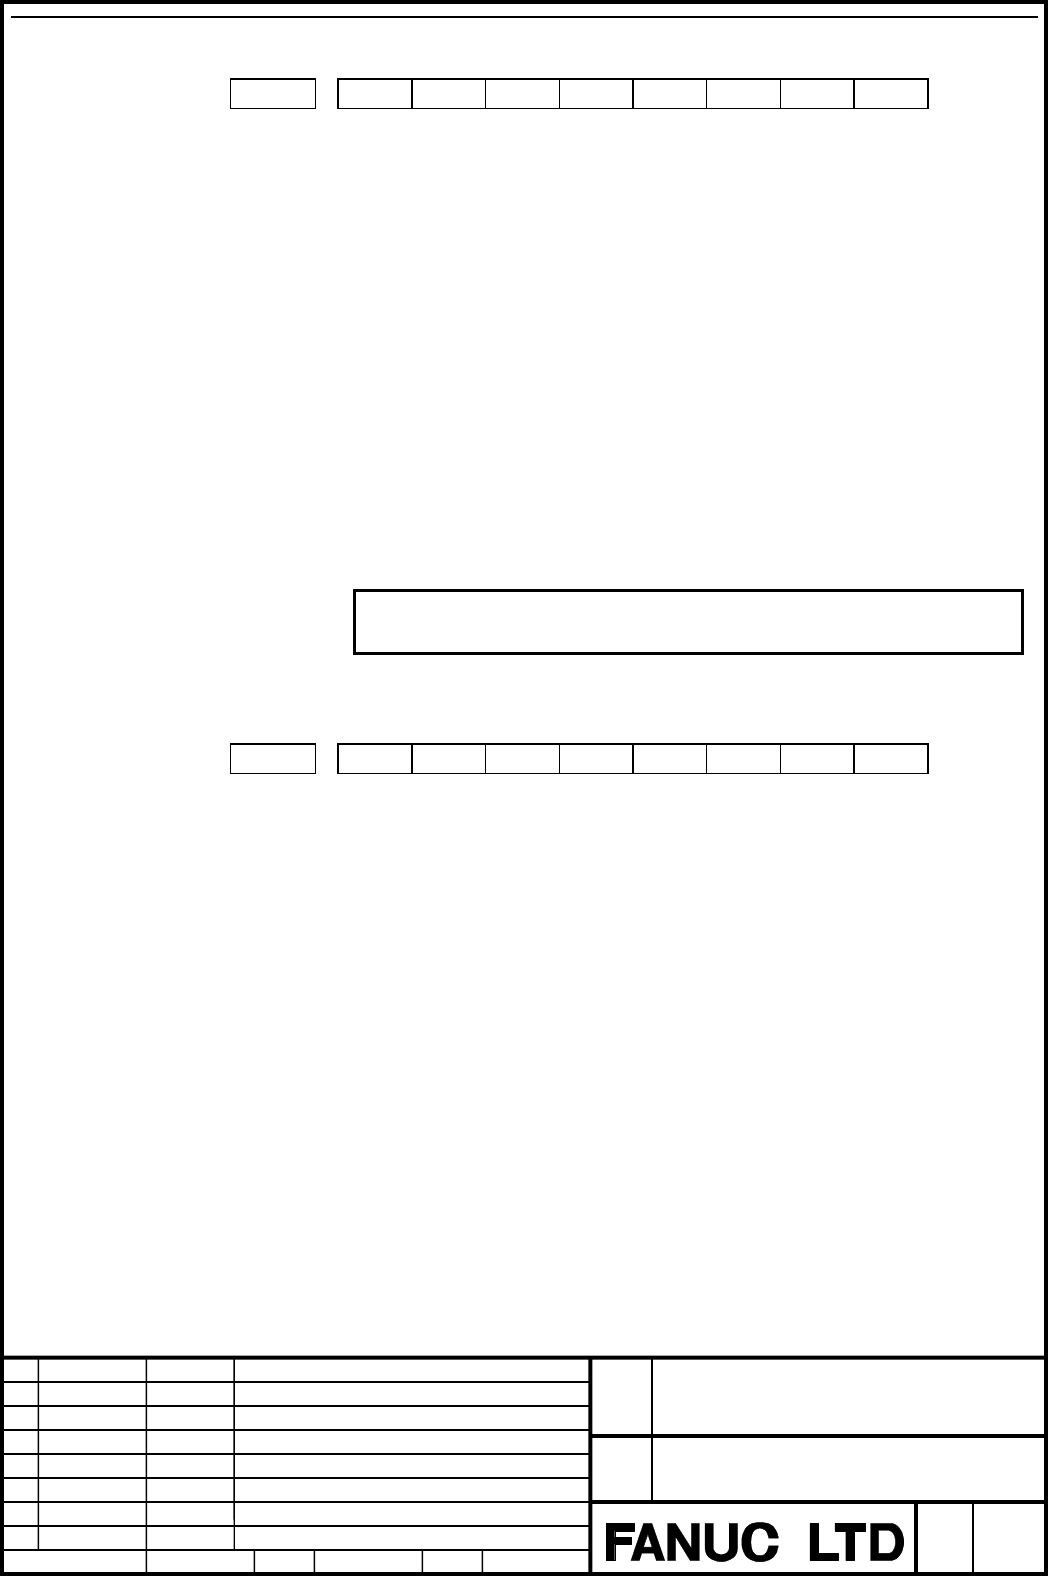
Parameter
#7 #6 #5 #4 #3 #2 #1 #0
1207 WOL
[Data type] Bit
WOL Calculation method of direct input of measured workpiece origin offsets is :
0 : Method-1
1 : Method-2
Method-1:
The workpiece origin offset value is measured with utilizing standard tool.
In this case, the value of tool length offset should be set the difference with a
standard tool length.
(The value of tool length offset for the standard tool must be 0.)
Method-2:
The workpiece origin offset value is measured with an arbitrary tool in consideration
of the tool length offset .
In this case, the value of tool length offset can be set the tool length itself.
NOTE
Method-2 is enabled only when bit 6 (DAL) of parameter No.3104 is set to 1.
#7 #6 #5 #4 #3 #2 #1 #0
3104 DAL
[Data type] Bit
DAL Absolute position
0 : The actual position displayed takes into account tool length offset (M series) or
tool offset (T series).
1 : The programmed position displayed does not take into account tool length offset
(M series) or tool offset (T series).
Edit
Apprv. Desig.
Sheet
Title
Draw
No.
Date
Design
Descri
p
tion
Date
FS 16i/18i– MB, 18i– MB5, 21i– MB
Improvement of Direct input of measured
workpiece origin offsets Specification
June.16.2004
02 2004/07/29 T.Mochida 2) part is added E.Genma
T.Mochida
E.Genma
4/5
A-79632EN
Contents Summary of Series 16i / 18i Additional Manual
- Page 1FANUC Series 16i / 18i – MB FANUC Series 18i – MB5 FANUC Series 21i – MB Improvement of Direct input of measured workpiece origin offsets Specification - Contents - OUTLINE............................................................................................................................. 2
- Page 2Outline Existing direct input of measured workpiece orgin offsets was an operation to set the workpiece origin offset value with utilizing a standard tool. This time, the method of the direct input of measured workpiece orgin offsets without utilizing a standard tool was added. Specifications Method
- Page 3Z0→[MEASUR] The value of workpiece origin offset for Z-axis is calculated so that absolute coordinate value of a tool tip is set to “0” by considering actual tool length offset. Therefore, the workpiece origin offset(G54(Z)) and absolute position(Z) becomes the following results. Actual workpiece or
- Page 4Parameter #7 #6 #5 #4 #3 #2 #1 #0 1207 WOL [Data type] Bit WOL Calculation method of direct input of measured workpiece origin offsets is : 0 : Method-1 1 : Method-2 Method-1: The workpiece origin offset value is measured with utilizing standard tool. In this case, the value of tool length offset sh
- Page 5Others - This function is effective in the following systems. 2) B0HA/BDHA/DDHA-16(P) or later (FS16i/18i/21i-MB) 2) BDHE-06(F) or later (FS18i-MB5) 2) FS 16i/18i– MB, 18i– MB5, 21i– MB Title Improvement of Direct input of measured workpiece origin offsets Specification Draw No. A-79632EN 02 2004/07